2022
1
Metal fabrication, Consumer industry
35 - 45 CW
10s/pc
Cat. 300k - 350k EUR
Handling, Measuring, Pressing, Assembly, Optical inspection, Camera guidance
Fanuc, Keyence, Siemens, Festo, Schunk, Flexibowl
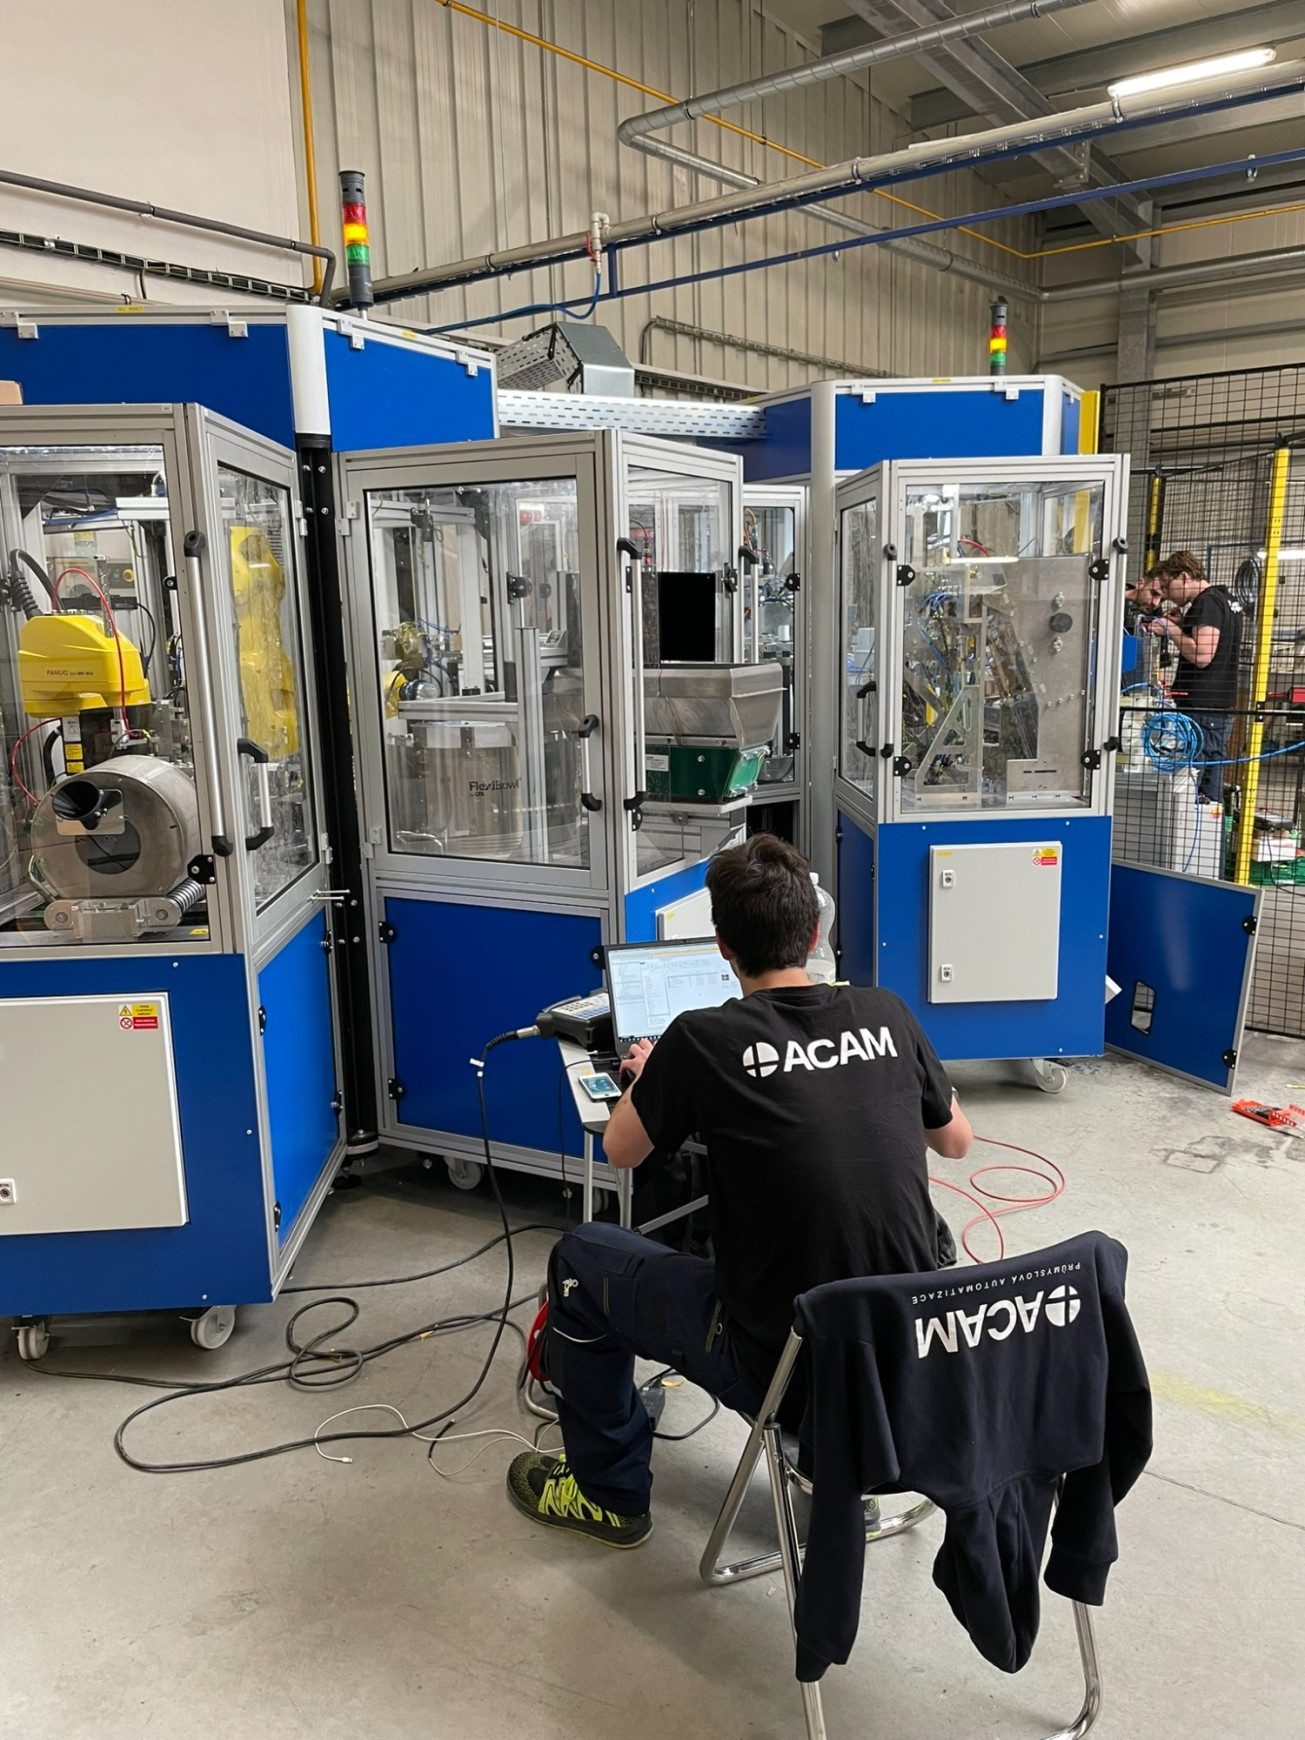
The customer specializes in the production of cylinders for fire extinguishers. Due to the nature of the final product - a part of the fire extinguisher, maximum attention is paid to 100% functionality of the device. Due to the enormous production volume, the requirement for zero tolerance of product error and the shortage of workers on the market, full automation of the process was resorted to. Due to the modernization of safety standards, the customer assessed the real risk of changing the production process. Given this need to react to possible changes in the future, the customer chose automation in the form of the HXG platform, which would allow them to react to changes better than a single-purpose machine.
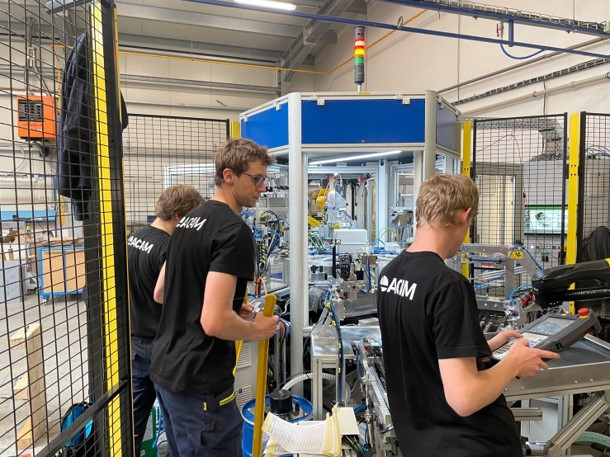
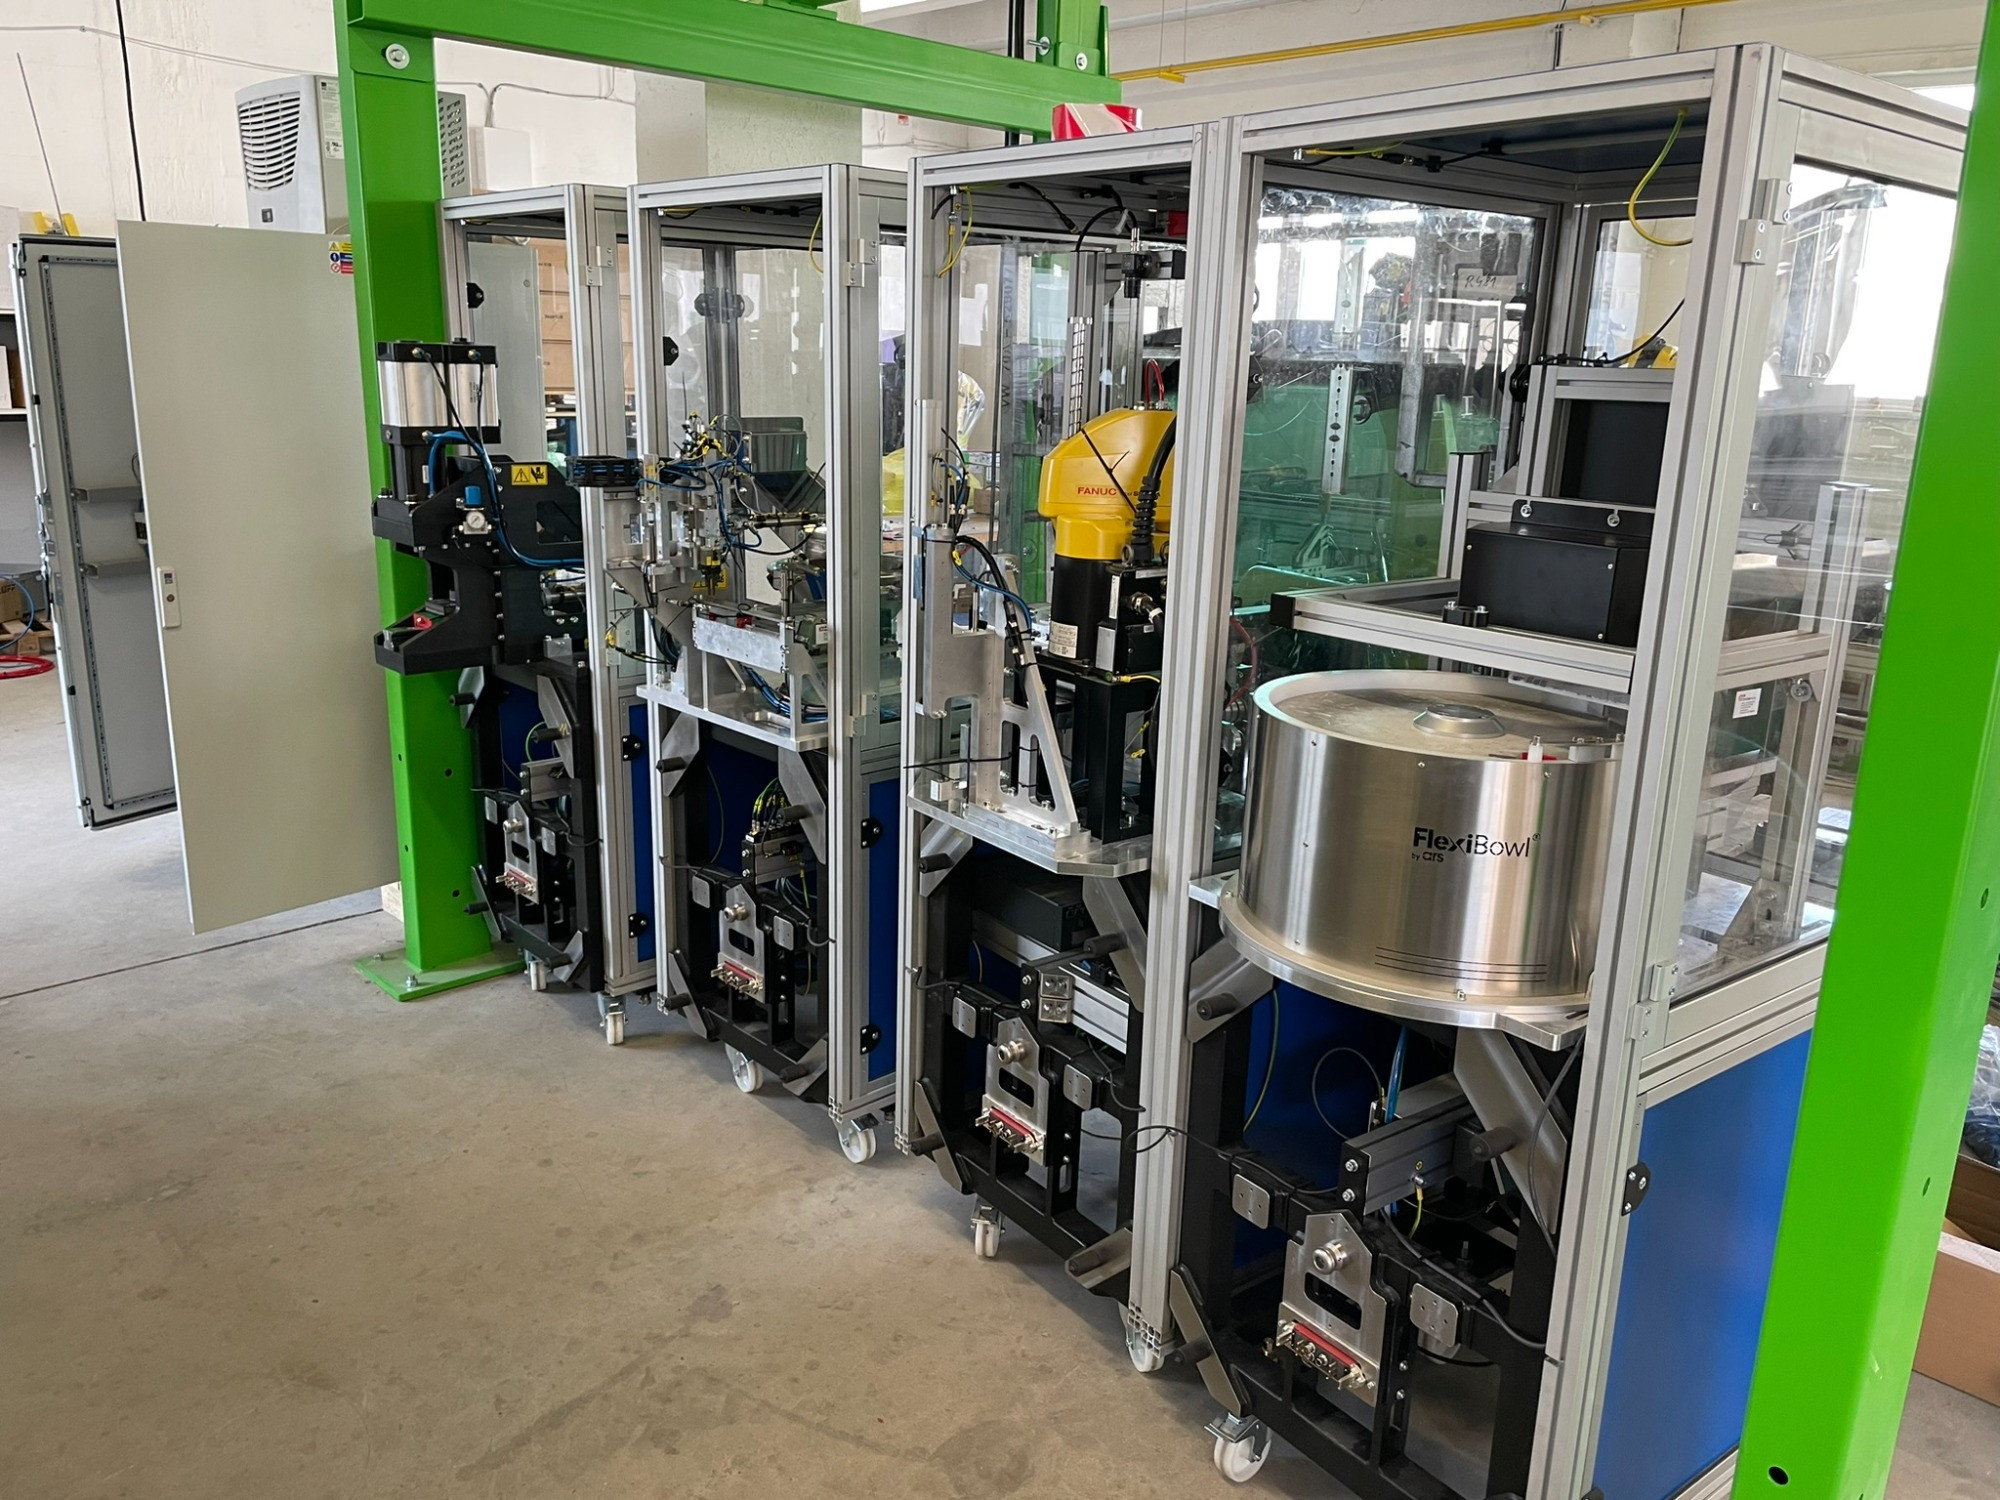
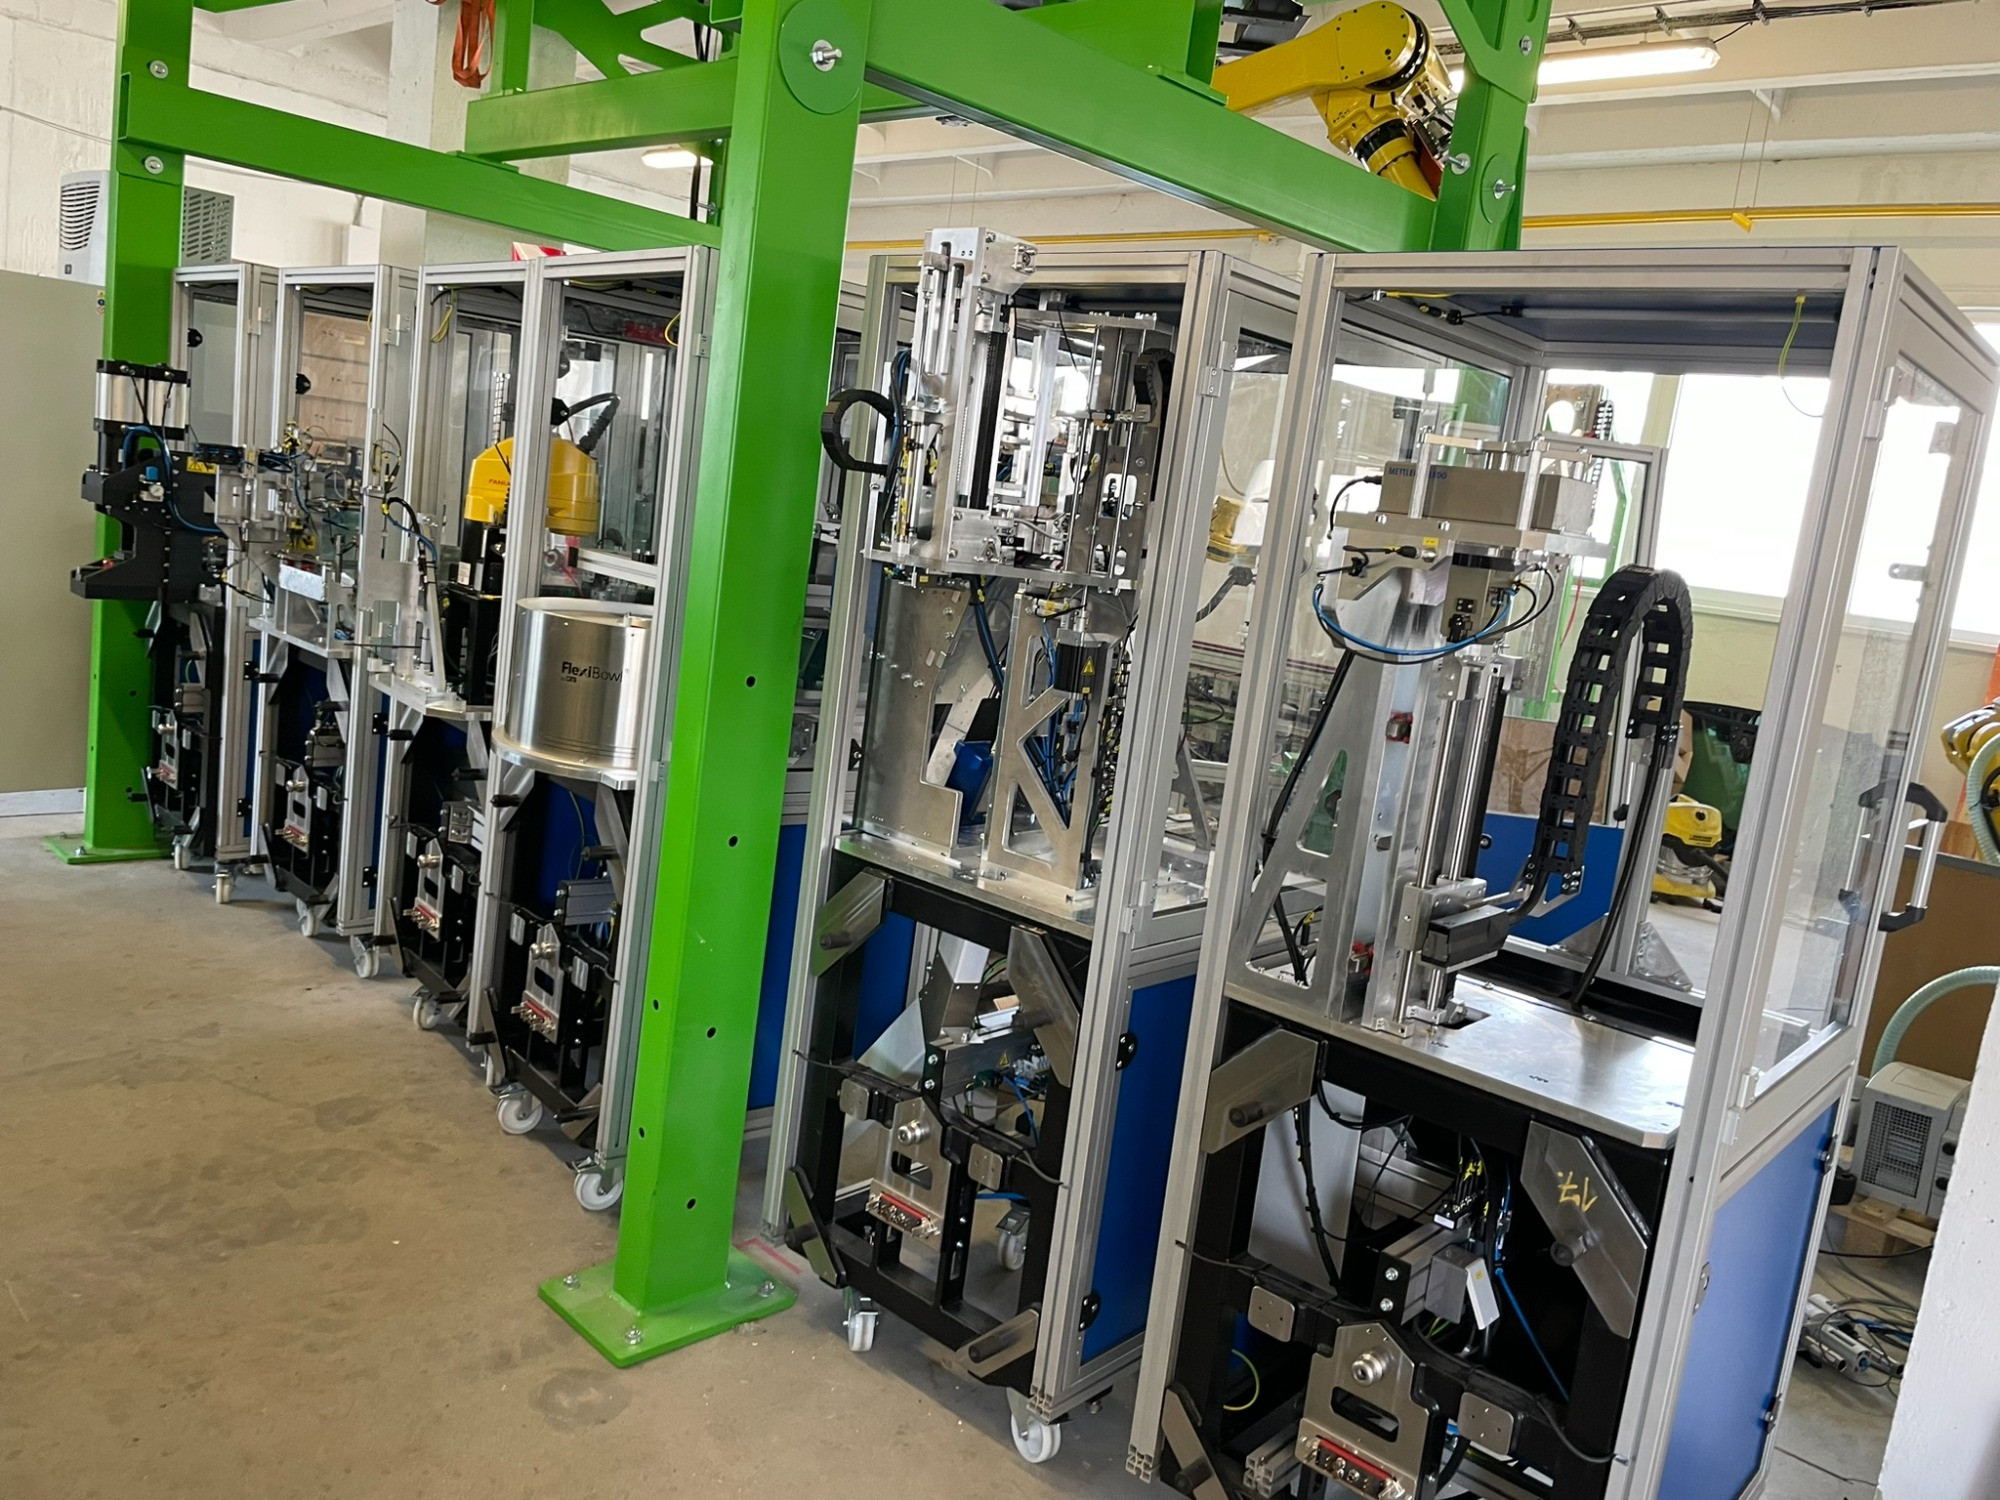
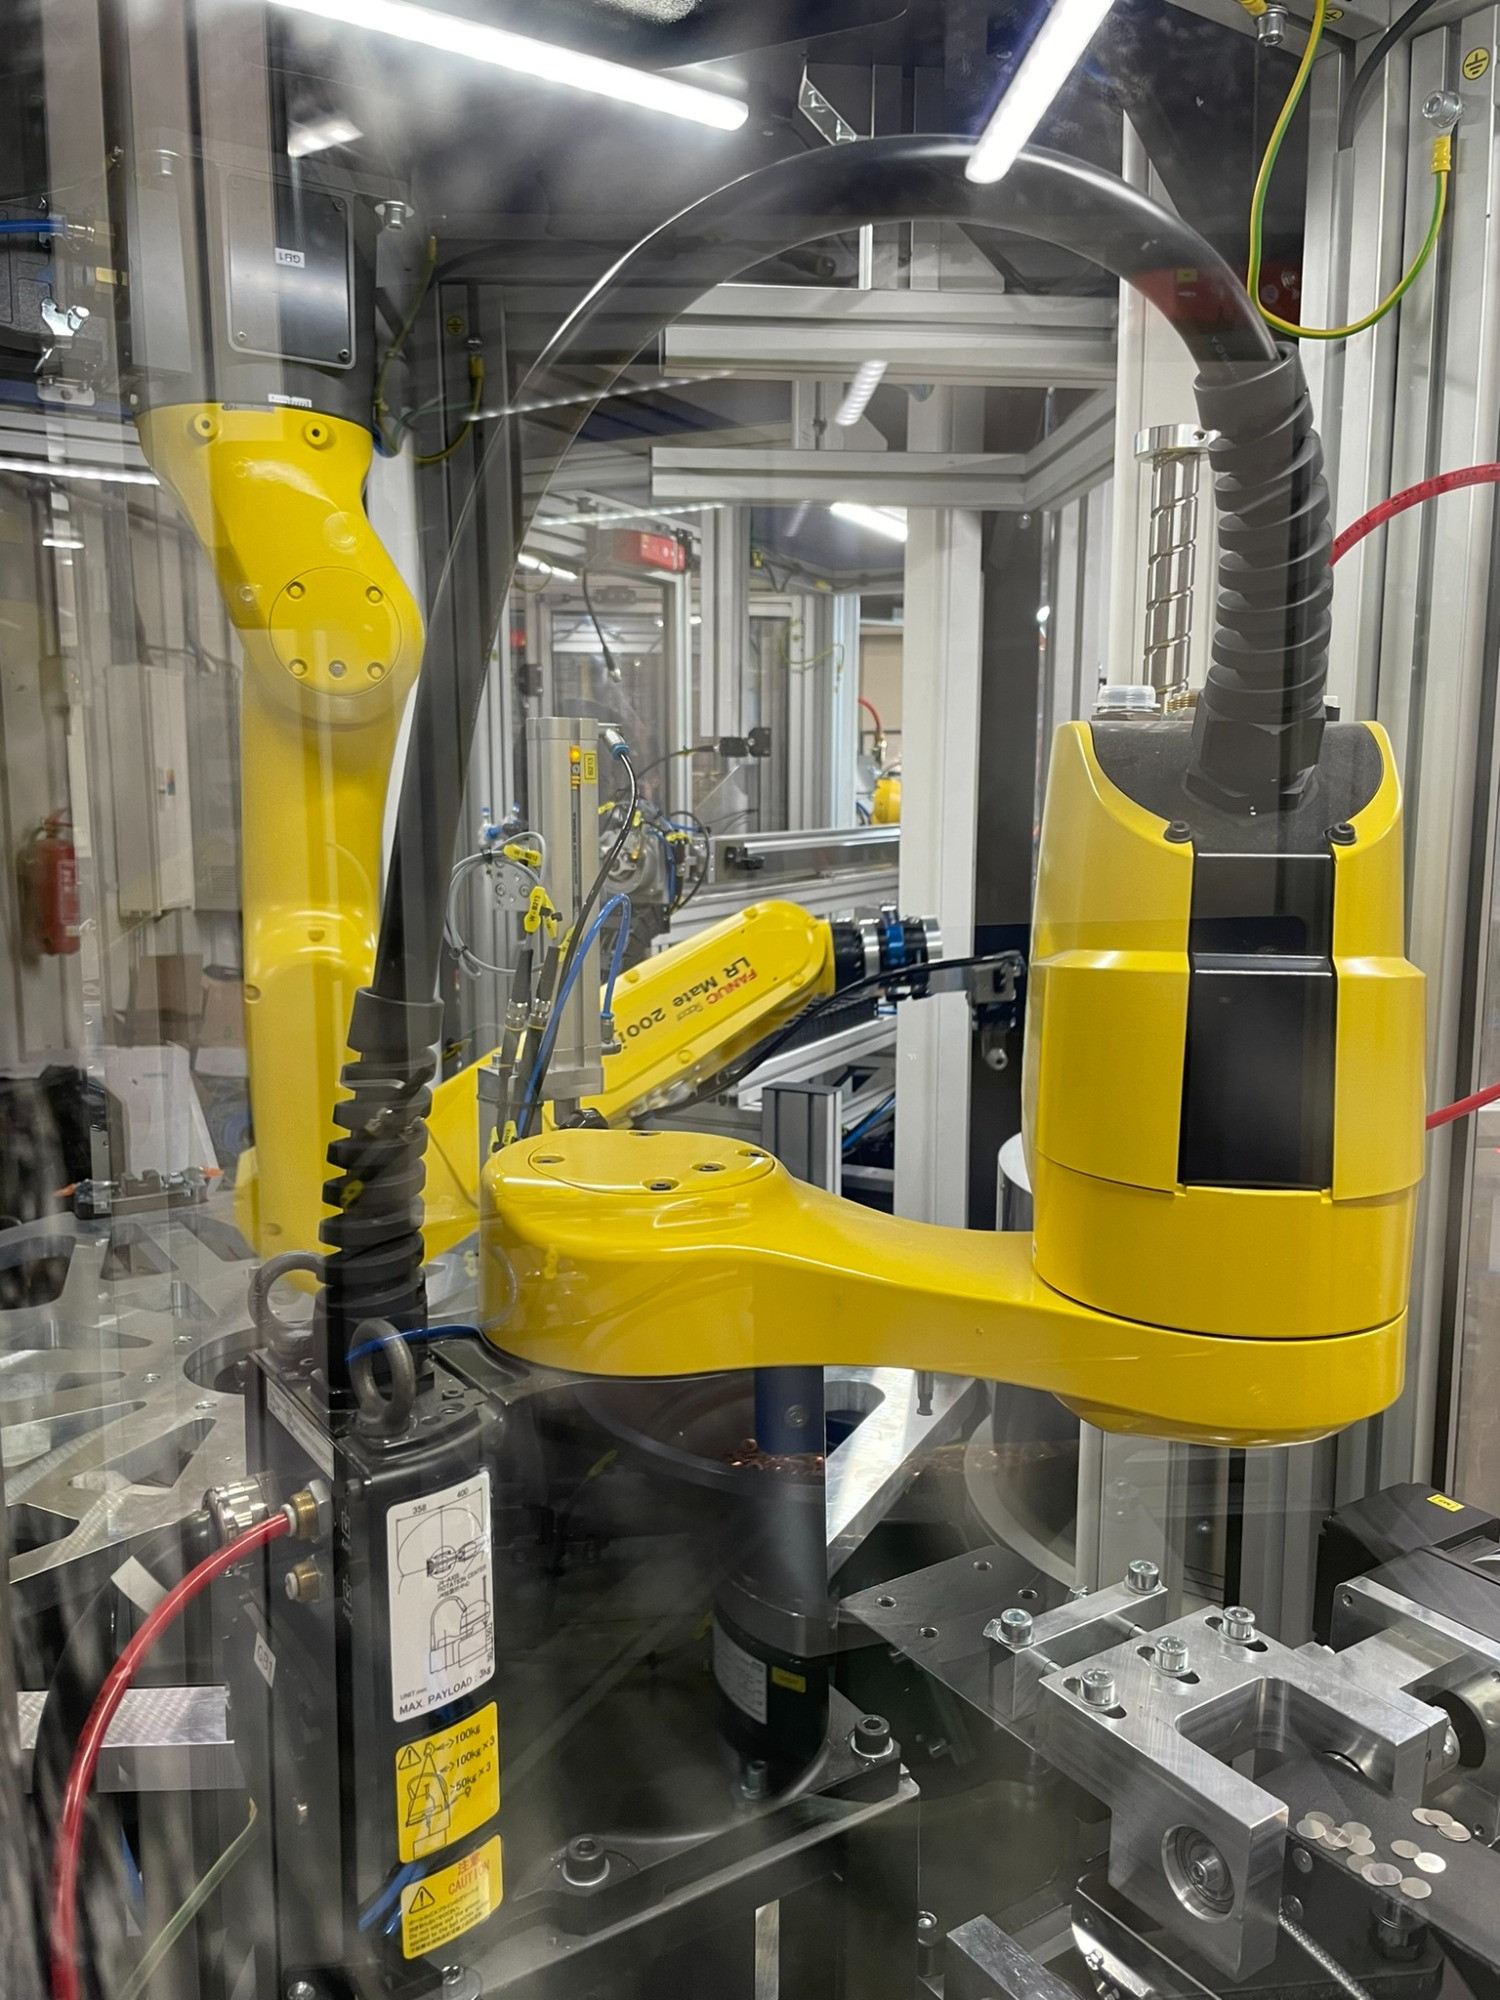
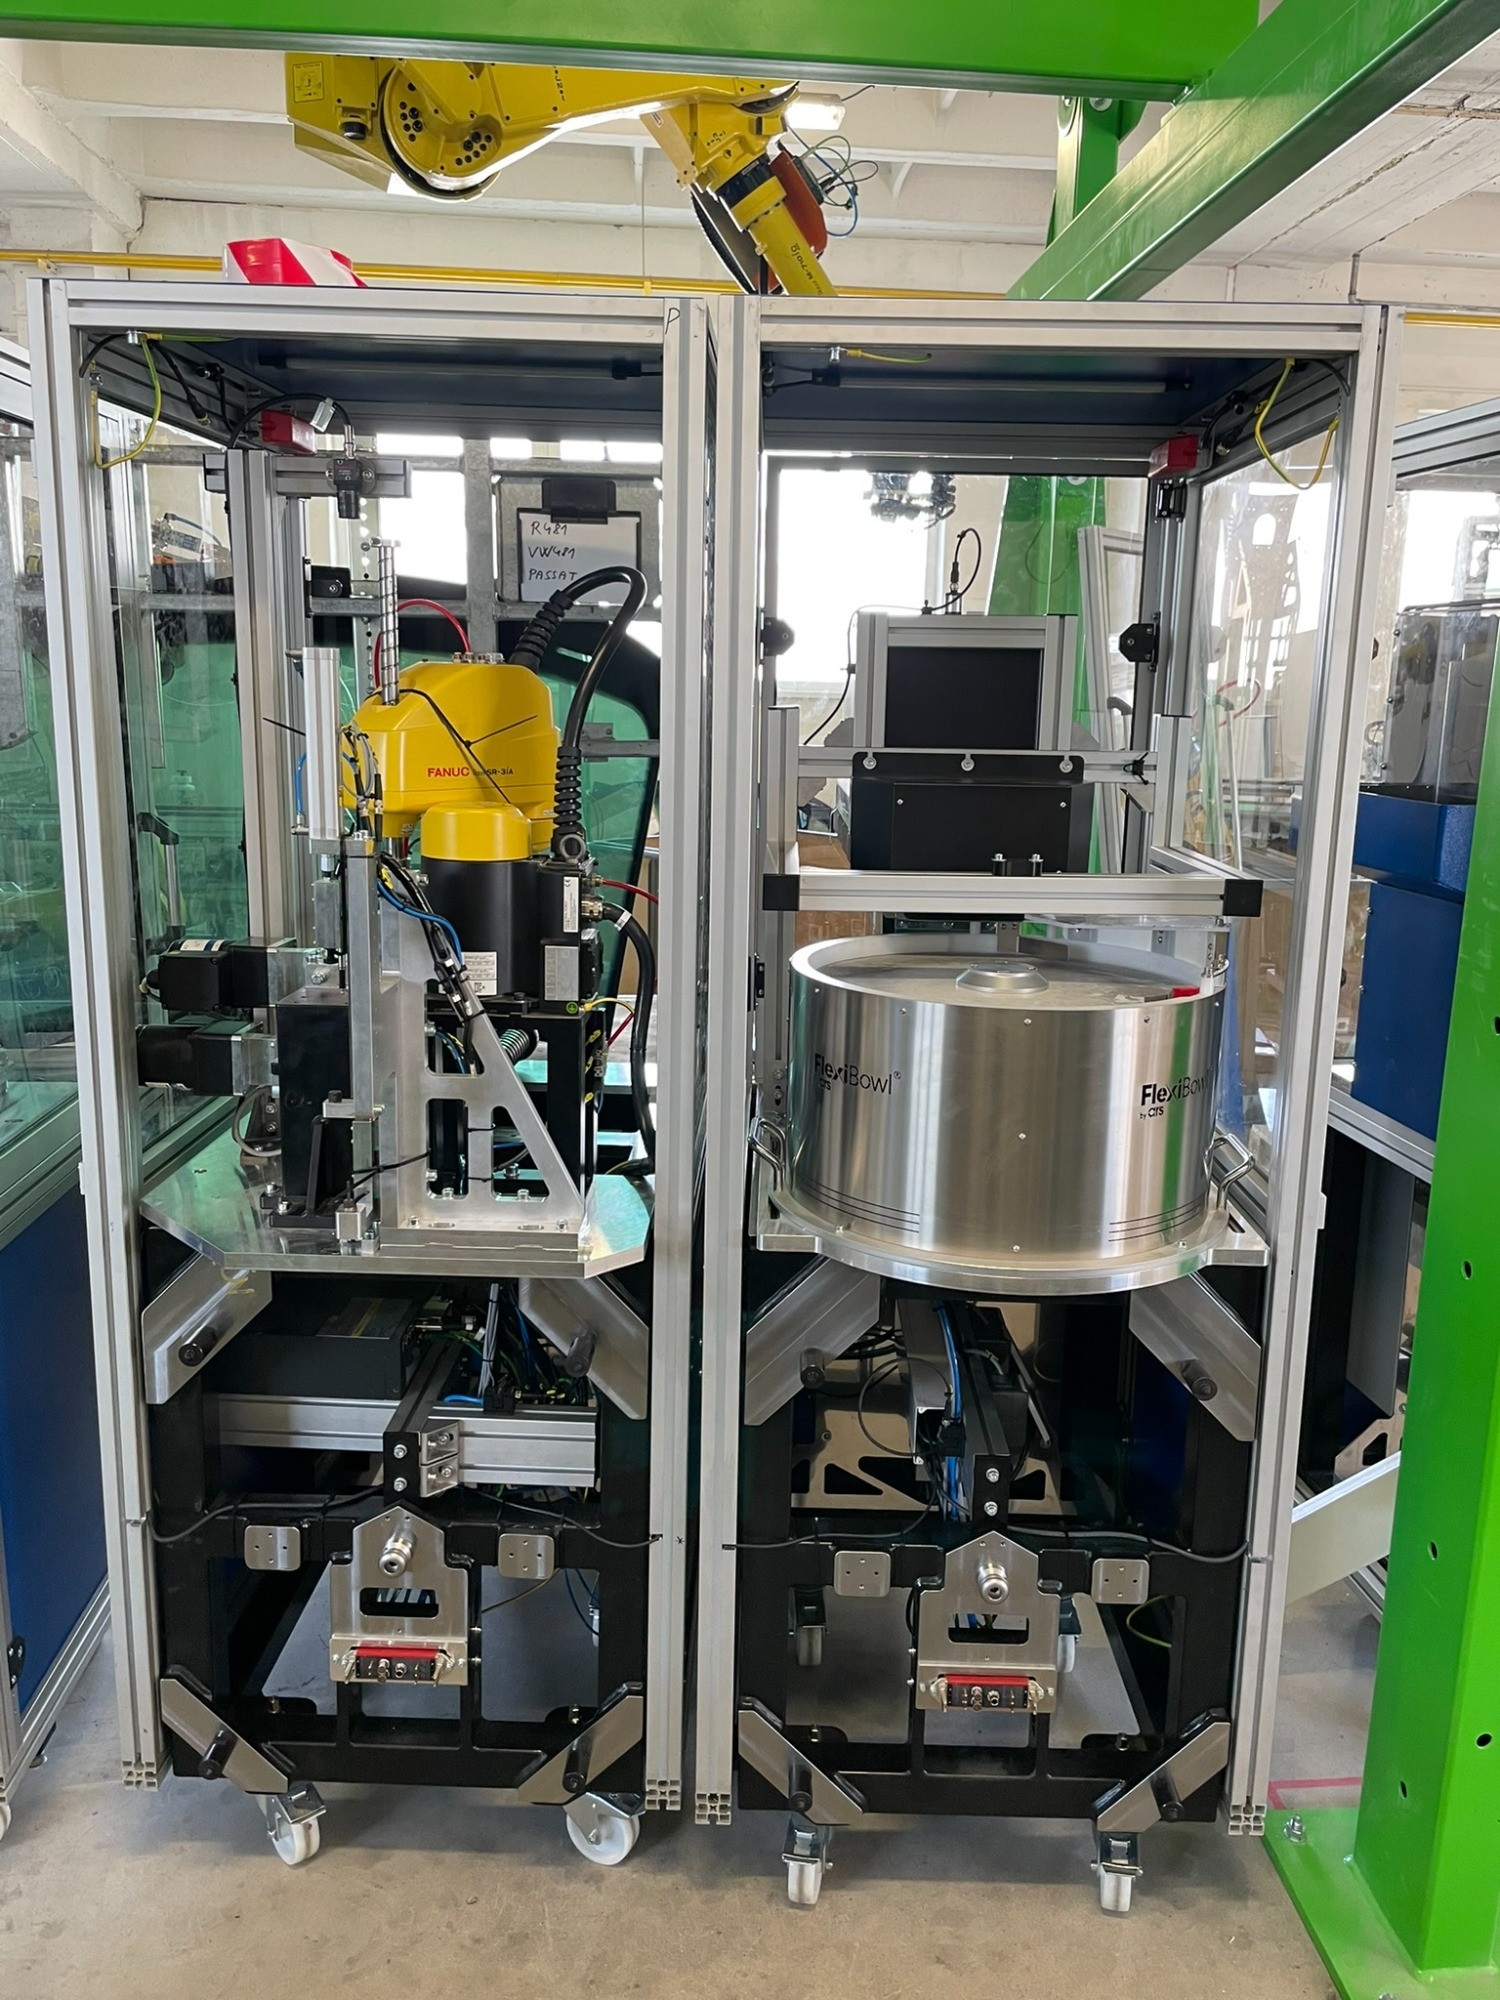
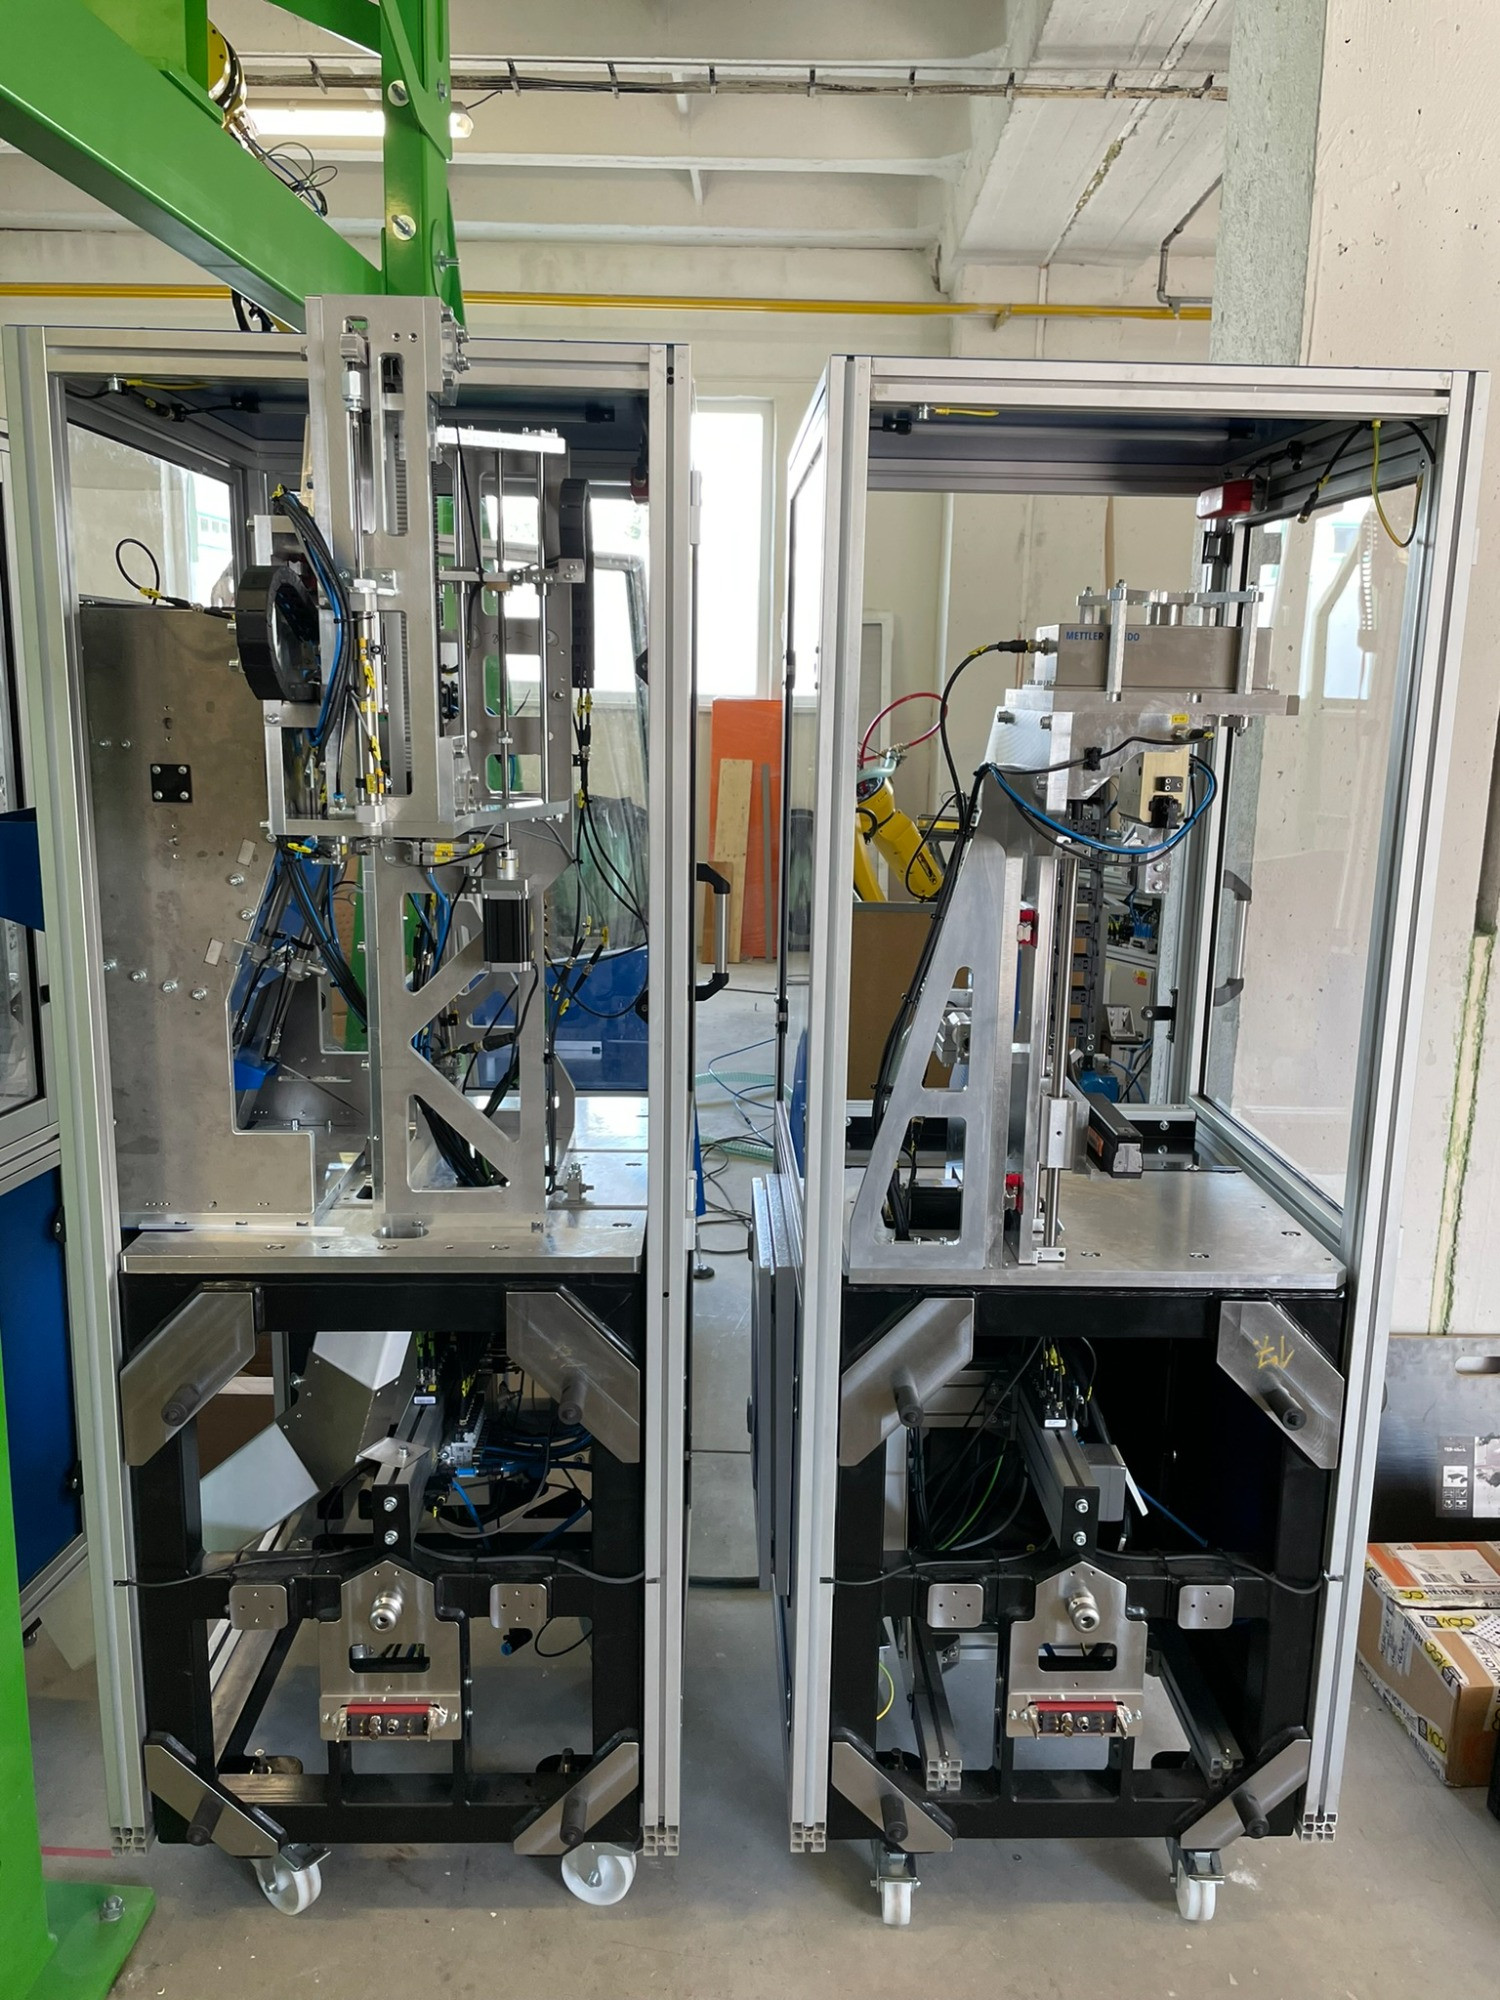
The subject of the implementation was the development and supply of equipment for the assembly of a family of valves for pressure cylinders with connection to an automatic cylinder filling process with assembly of the manufactured valves. The equipment can work both in cooperation with the production line and independently for the production of valves as spare parts for manual assembly.
In view of the customer's need for rapid response to change and a broad product portfolio, the equipment was designed on the HXG platform - a reconfigurable robotic platform in configuration:
Process Description:
Whether you are looking for a supplier of complex system integration, a specific service, or simply need advice.

Each project is unique, but they are all united by automation. It gives you an idea of our capabilities, whether it's robotic applications, our HXG platform, control and single-purpose equipment. We can automate anything.


This site is protected by reCAPTCHA and the Google Privacy Policy and Terms of Service apply.
